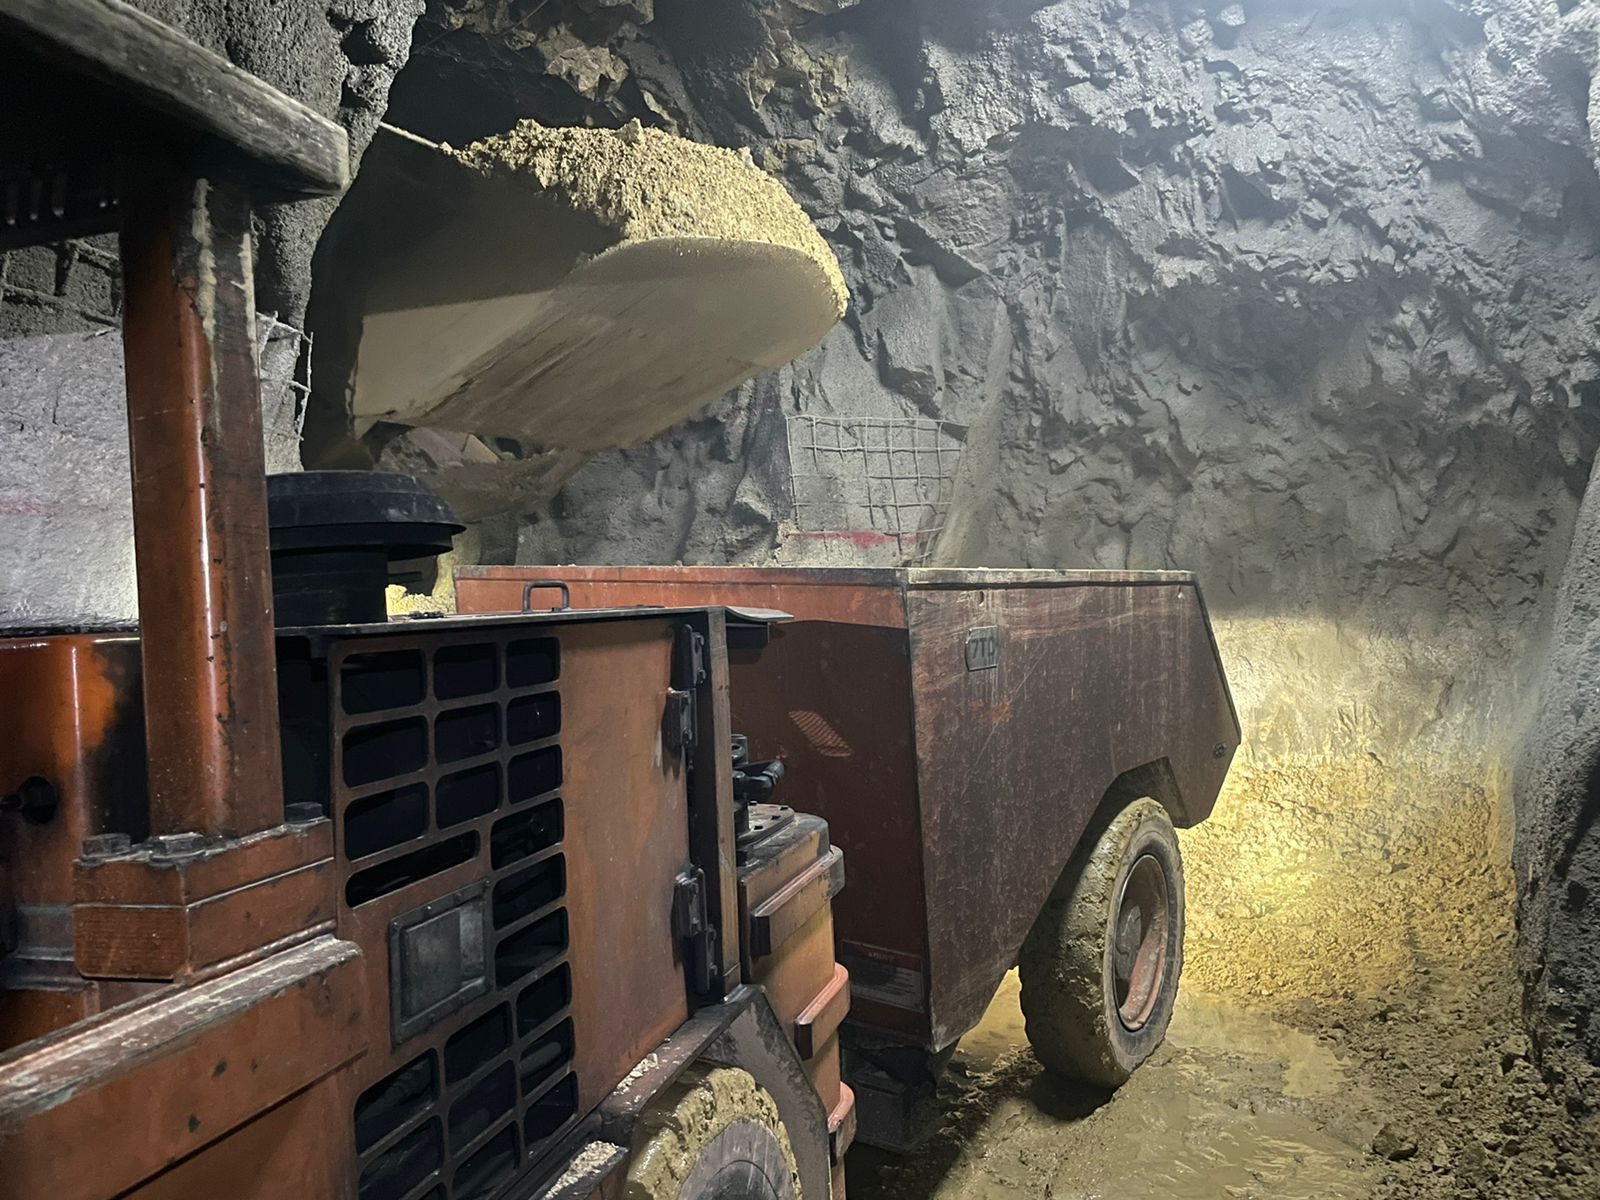
Mucking & hauling equipment
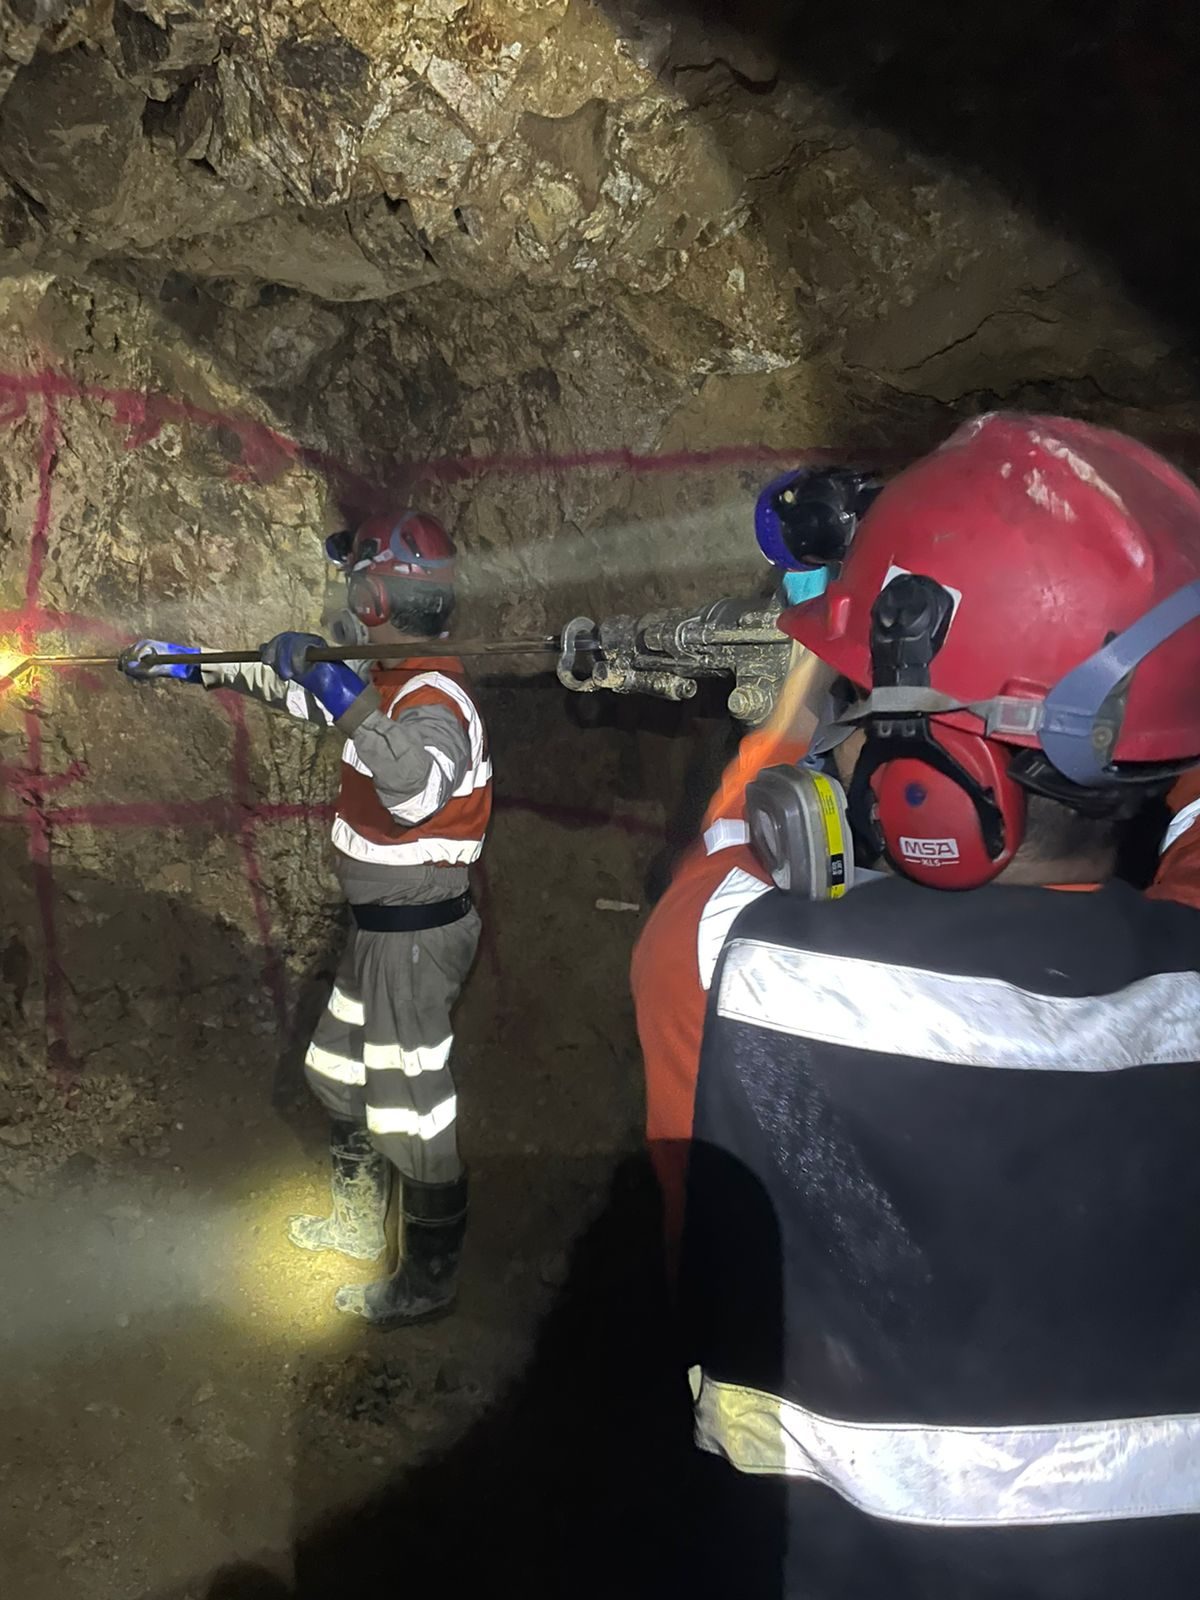
New mucking and hauling equipment brought into the mine.

Rochester Resources is improving silver recovery at its long-running Mina Real operation in Nayarit, Mexico, with a new pretreatment circuit and a revamped mine and plant.
The opportunity
Mina Real’s mineralized material carries a naturally high manganese content. Manganese occludes silver and interferes with conventional cyanide leaching, which historically limited silver recovery.
Already mined.
Already crushed.
Over many years of operation, the company has accumulated significant tonnage of mineralized material in its tailing impoundment areas. With the upgraded mill now able to handle the higher manganese content, processing this material is a focus for fiscal 2027.
Recovery
In 2024, a laboratory testing program with the University of Guanajuato identified a pretreatment ahead of conventional cyanidation. A three-month industrial pilot at the plant confirmed the lab work. In fiscal 2026, reported silver recovery was 66.70%, up from 52.98% in fiscal 2025.
Historical baseline, industrial pilot and reported fiscal-year results
Fiscal-year figures are reported plant results from the MD&A for the year ended May 31, 2026. Gold recovery was 99.60% in fiscal 2026 (fiscal 2025: 96.76%). Pilot figures are from a three-month industrial pilot.
From lab to plant
A laboratory testing program, in partnership with the University of Guanajuato, evaluated mine mineralized material, tailings, and blends of both.
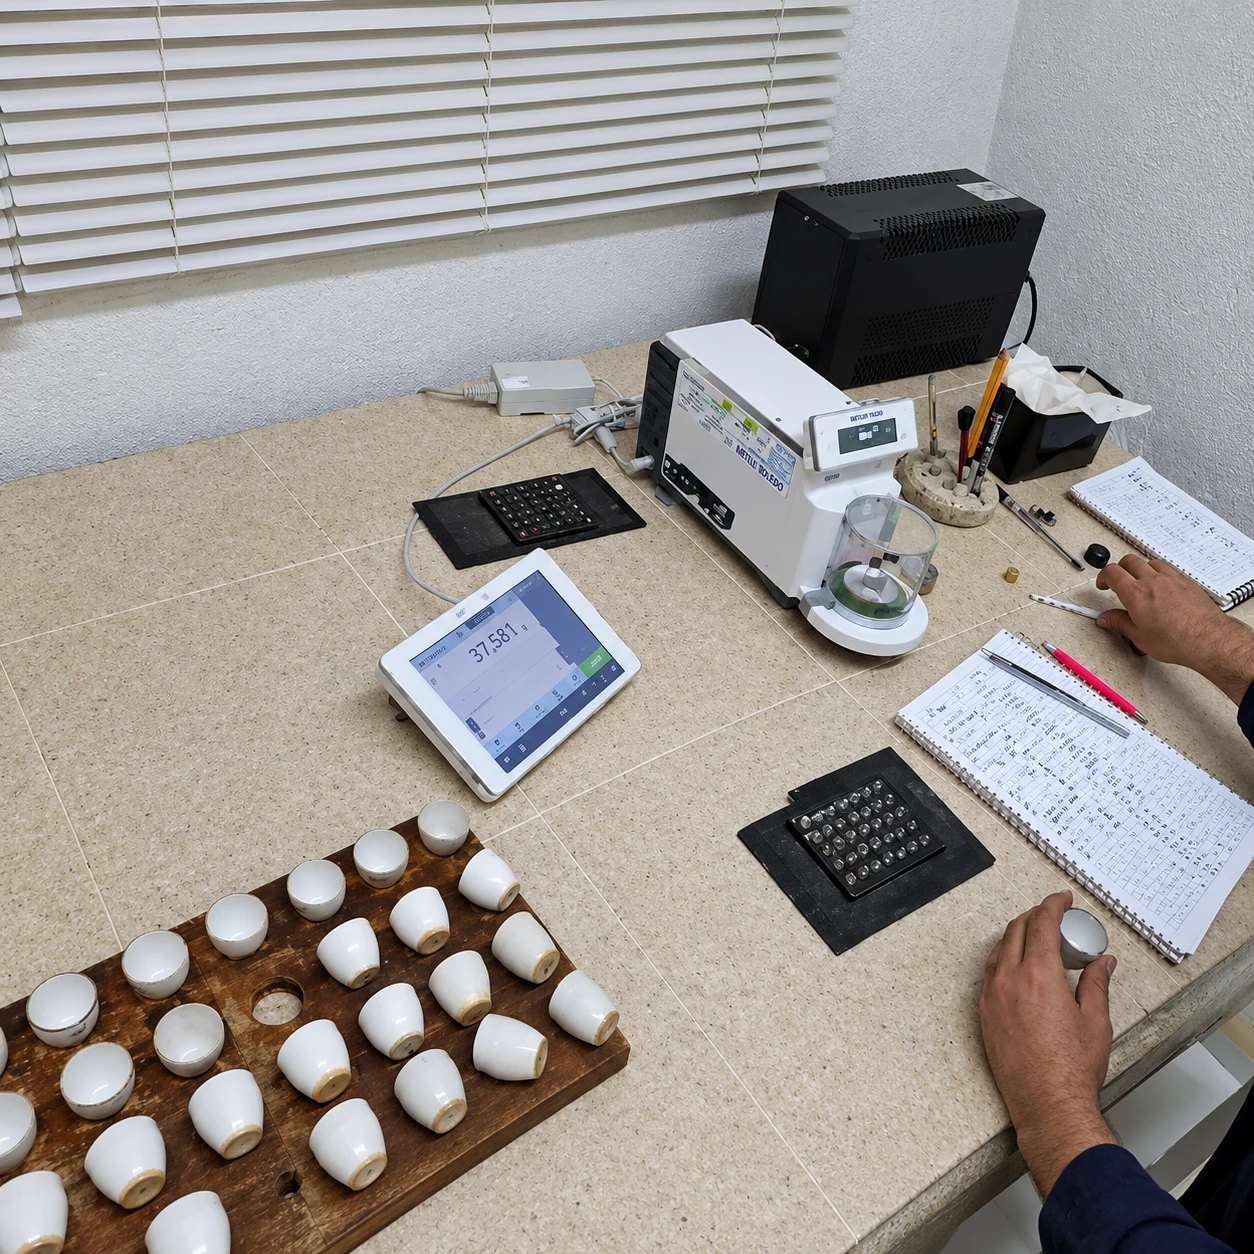
Testing identified a pretreatment of ammonia bisulfite and sulphuric acid ahead of conventional cyanidation, with substantial improvements in recoveries.
A three-month industrial pilot at the plant confirmed the lab work: 62% silver recovery from mine mineralized material and 56% from tailings.
A conceptual engineering study defined a full-scale circuit sized for 500 tons per day of tailings alongside 160 tons per day of fresh mineralized material.
Engineering, permitting, procurement and construction were carried out over the course of 2024, with plant modifications beginning in October 2024.
The new circuit commenced operations on March 21, 2025.
Revamping Mina Real
With the design in place, the company carried out a comprehensive revamp of both the mine and the plant.

New mucking and hauling equipment brought into the mine.
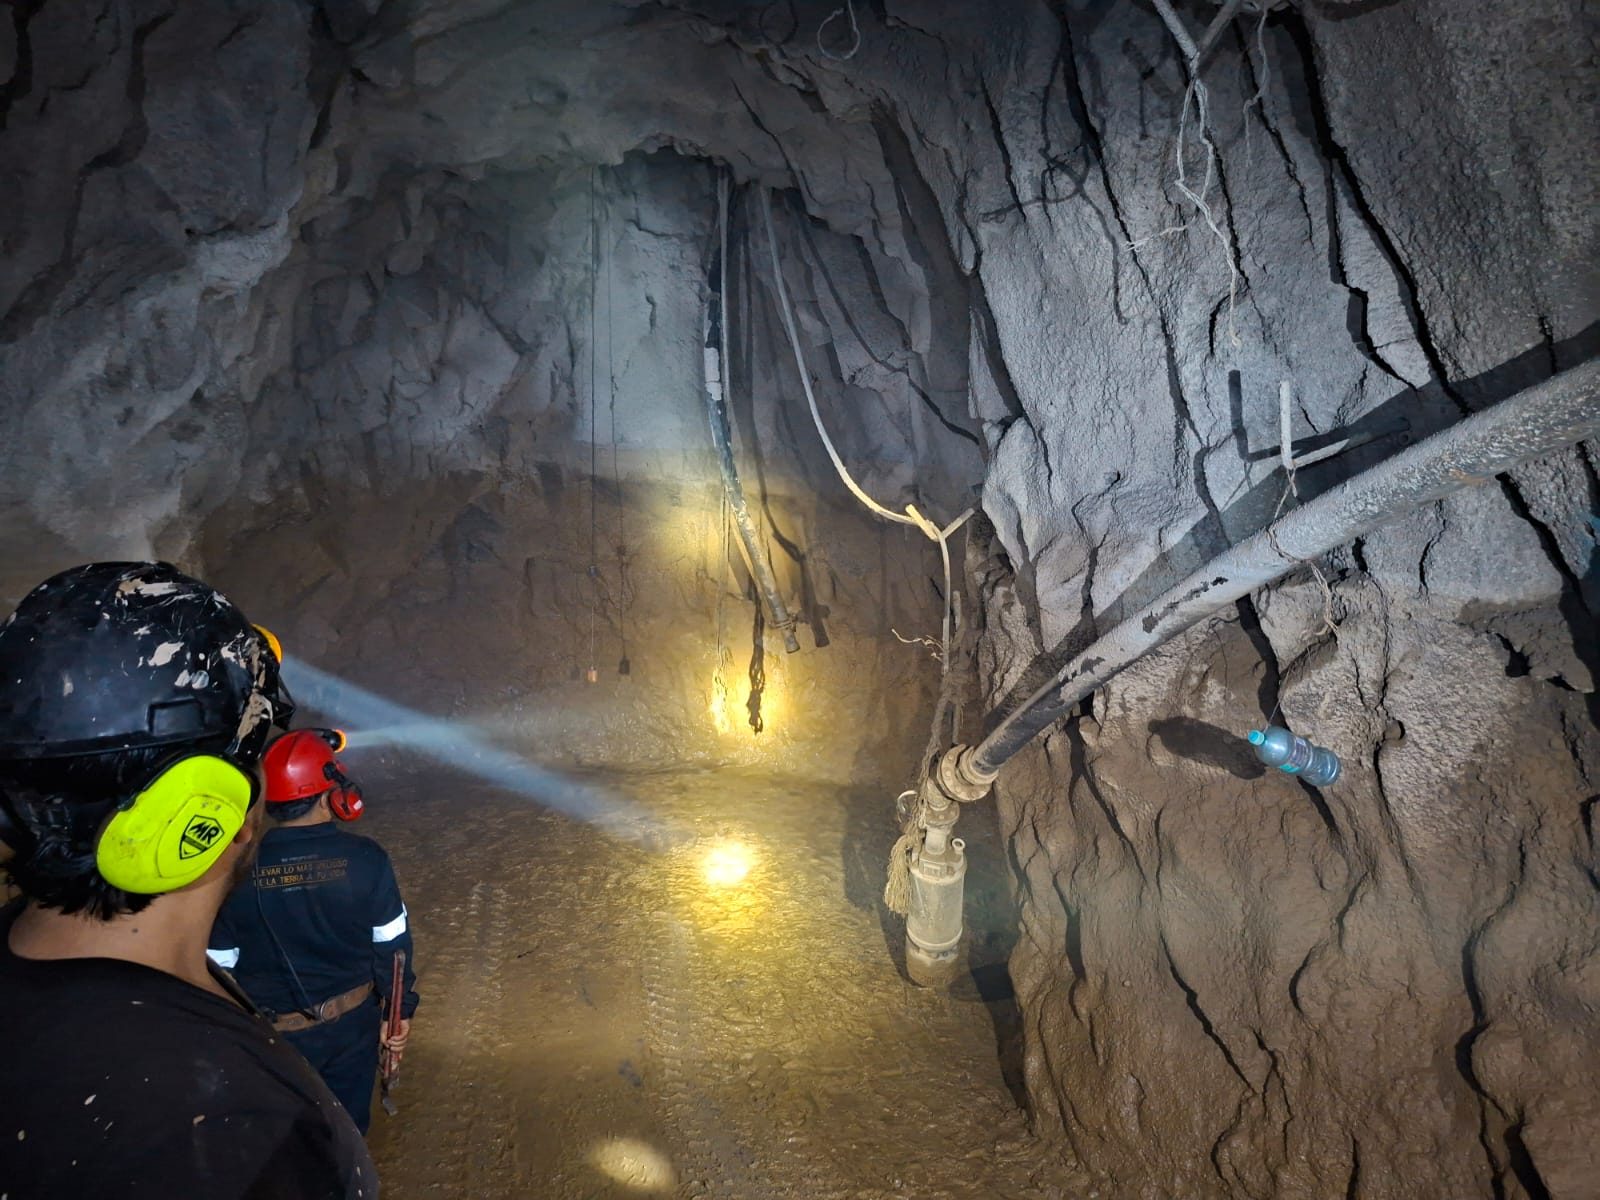
Mine water pumping stations rehabilitated, including cleaning of sump 018.
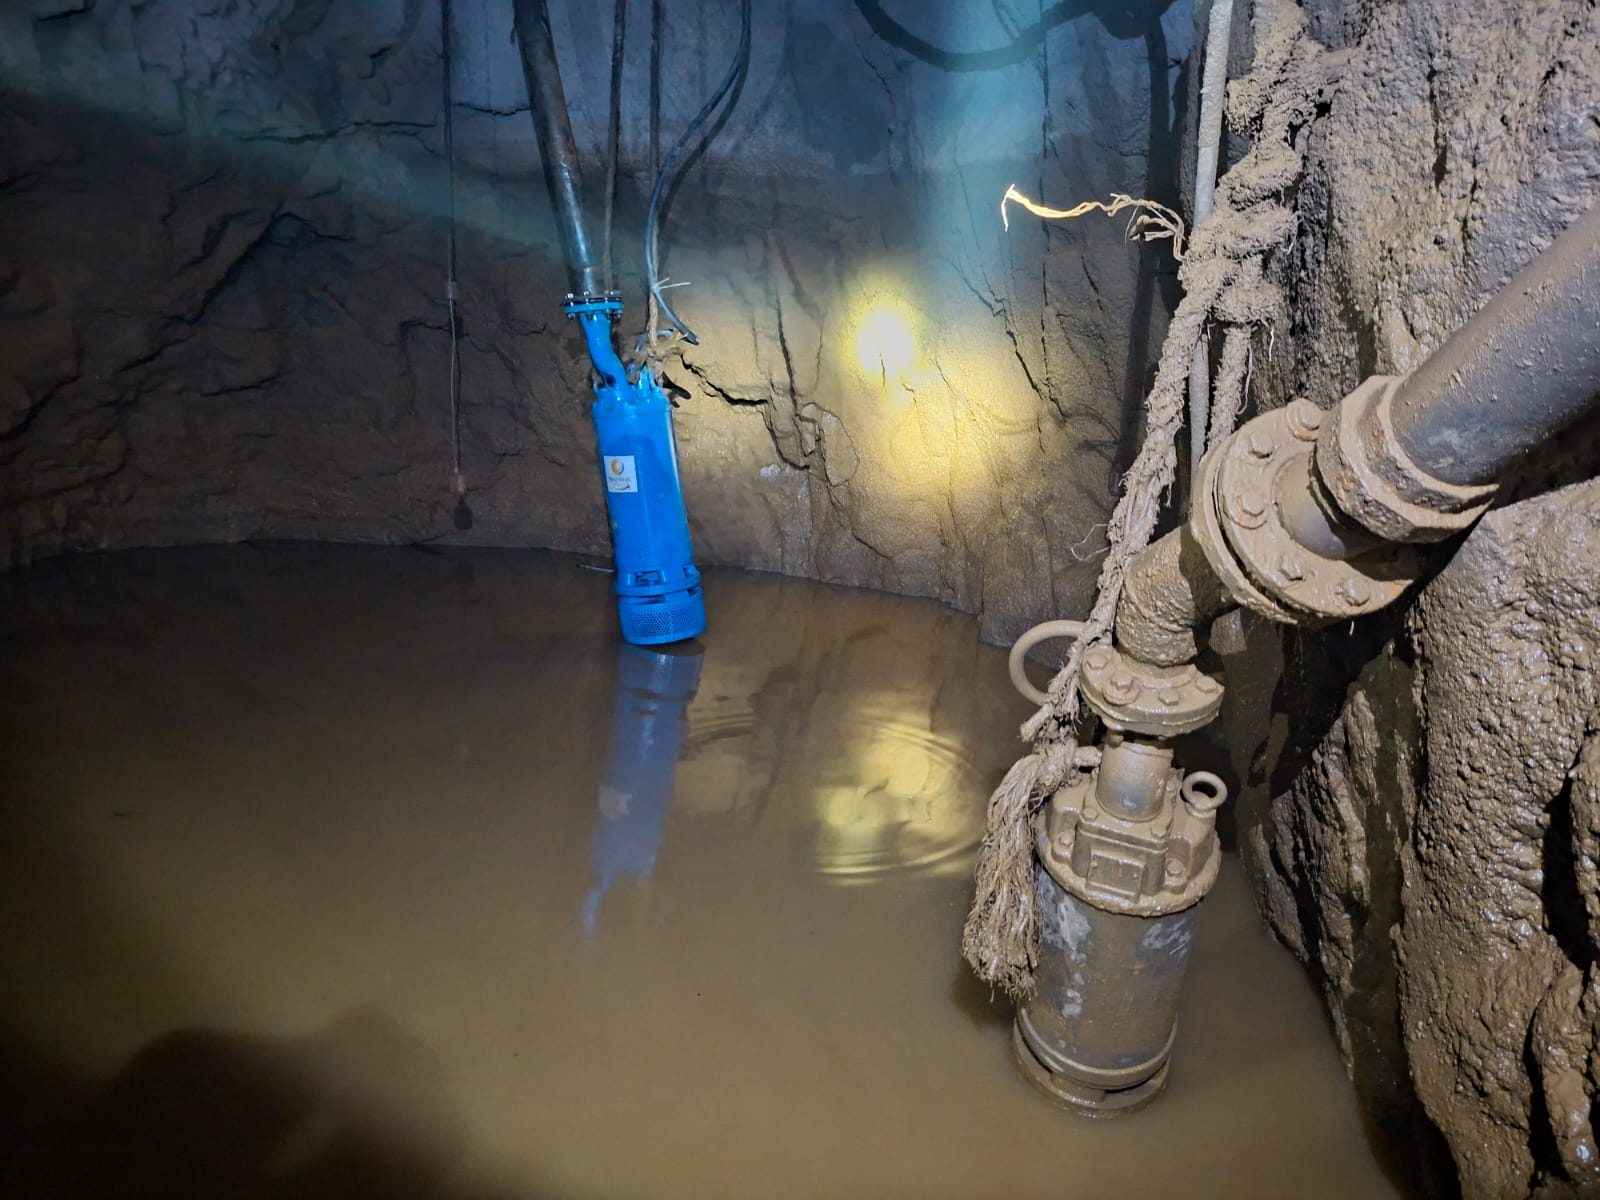
New pumps installed, including a 40 HP pump at sump 018.
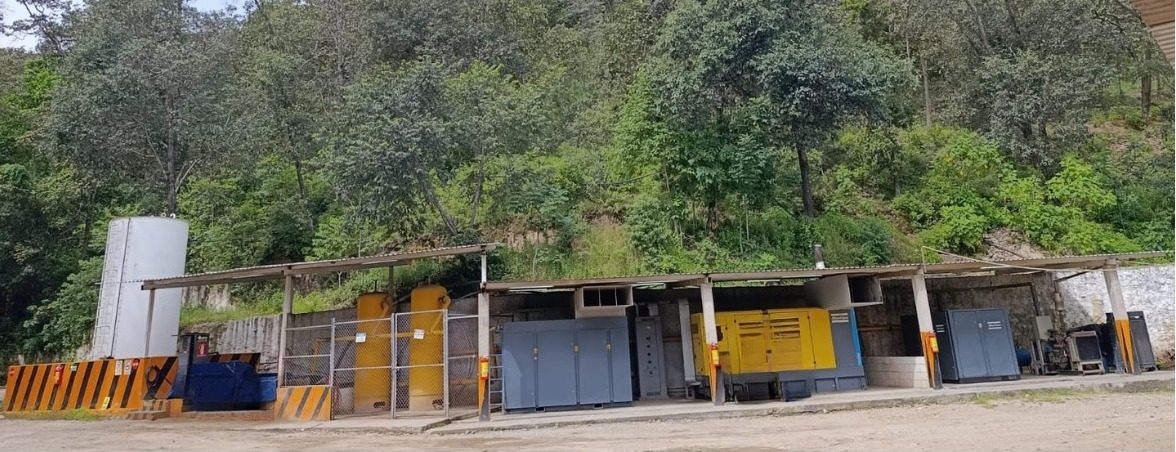
Mine electrical systems upgraded.
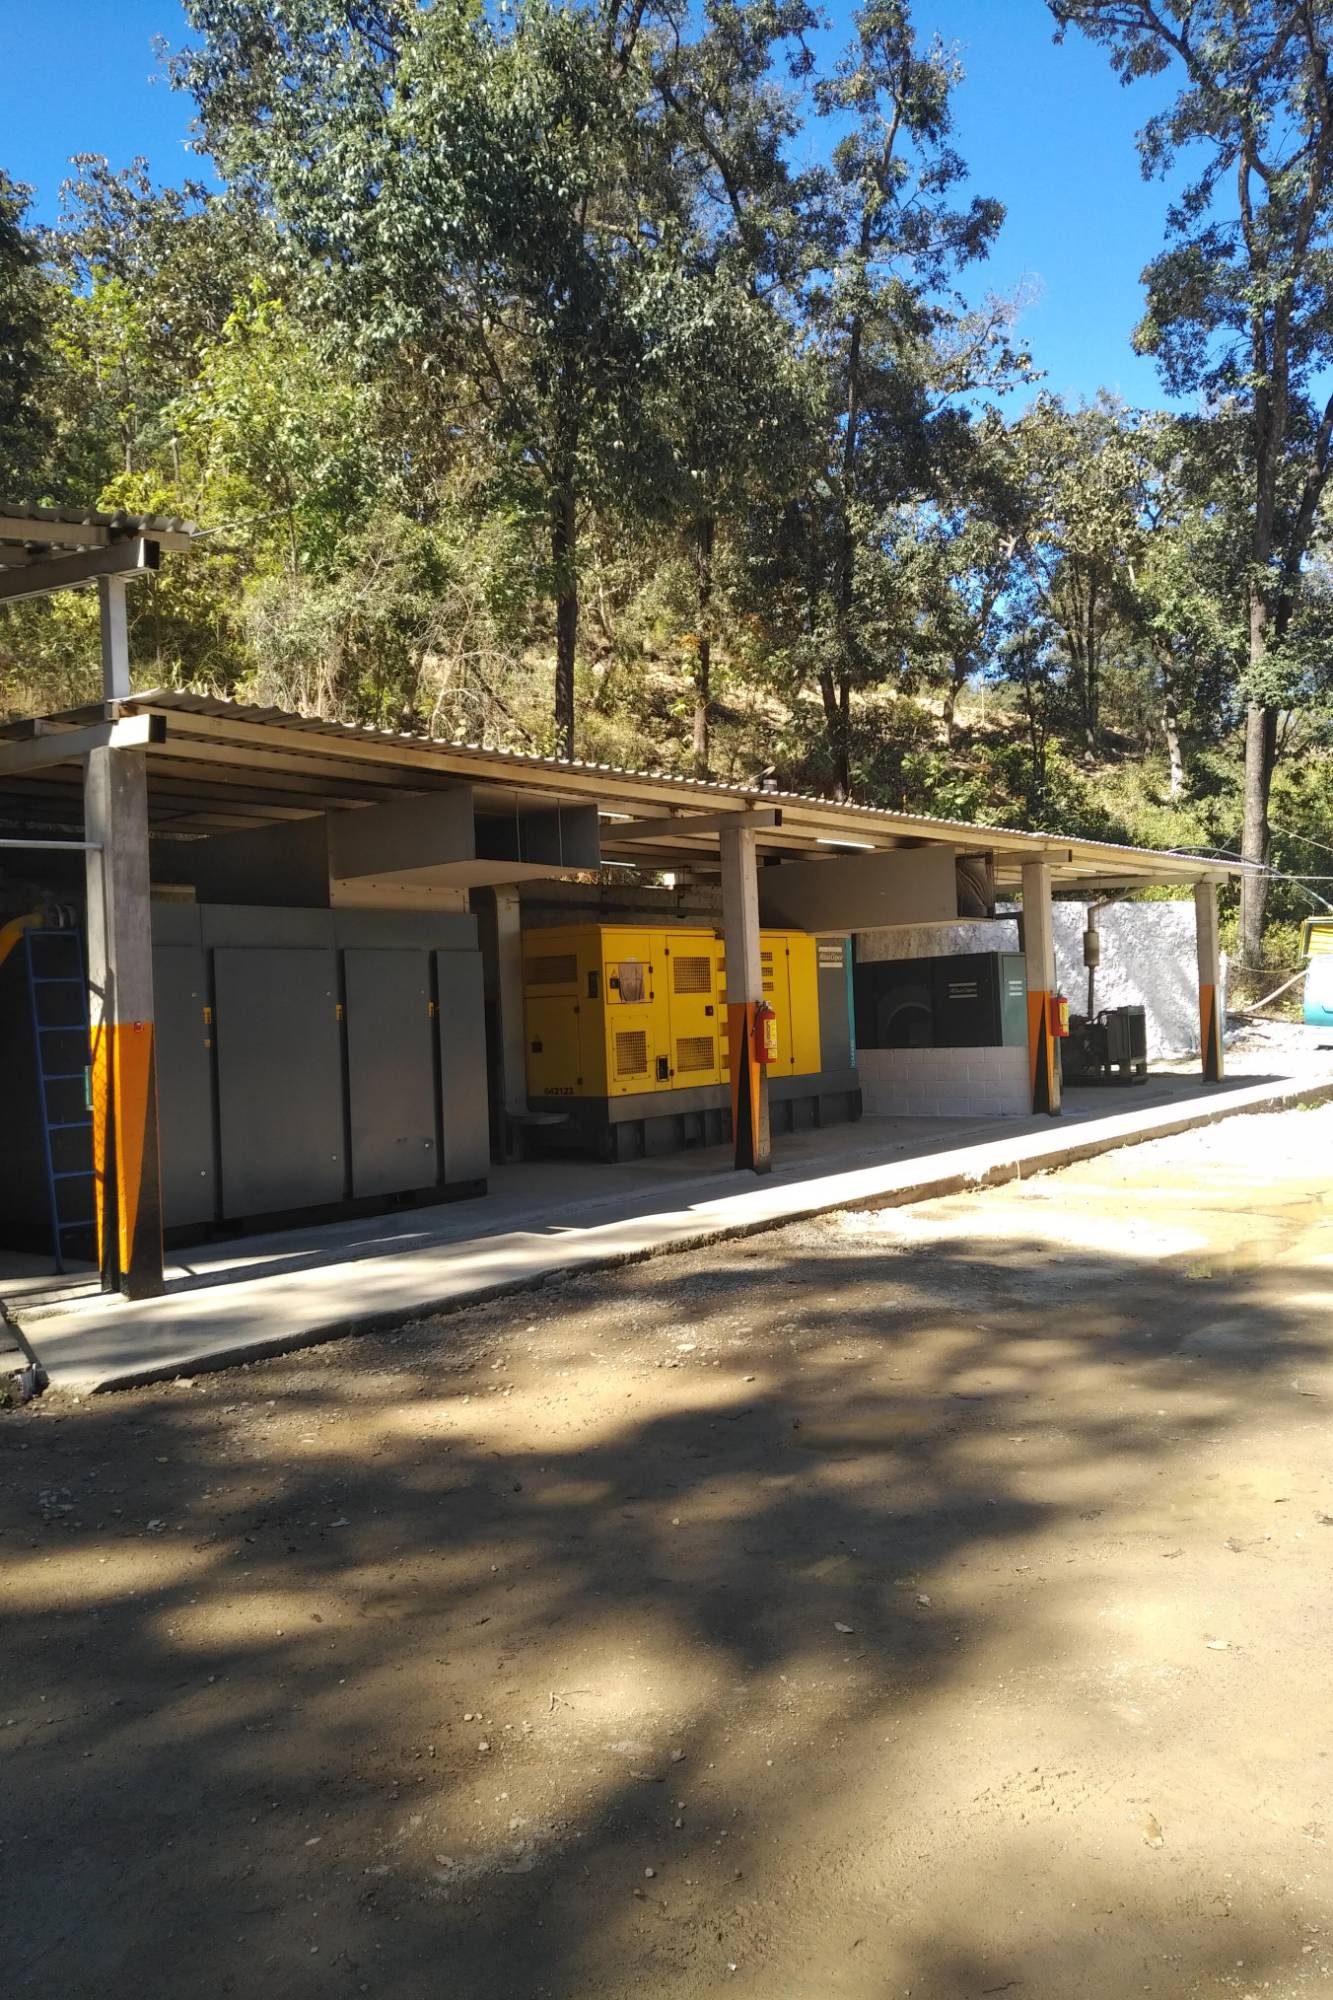
Mine compressed-air systems upgraded.
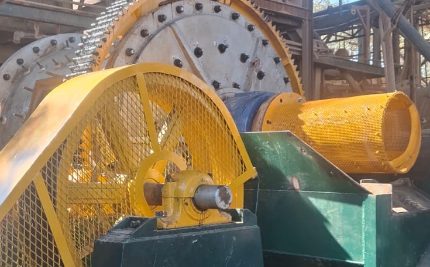
After the 6′ × 5′ mill went out of service in October 2025, the company sourced a used 6′ × 6′ mill, rebuilt and installed it, with a corresponding slurry pump upgrade. It was commissioned and began operating in late December 2025.
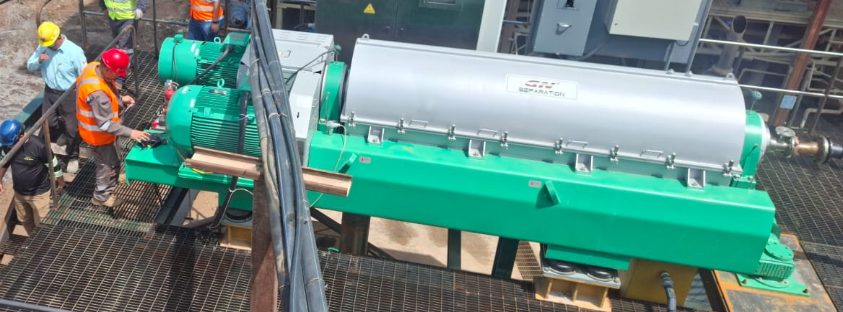
A high-speed centrifugal decanter for liquid-solid separation, installed and started up, recovers water, residual values and cyanide for reuse.
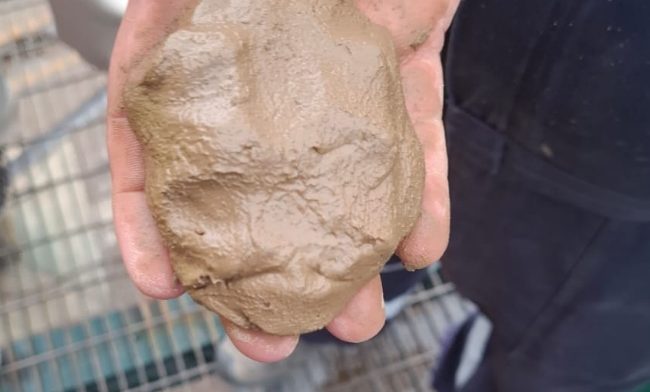
Water is recovered by the centrifugal decanter for reuse.
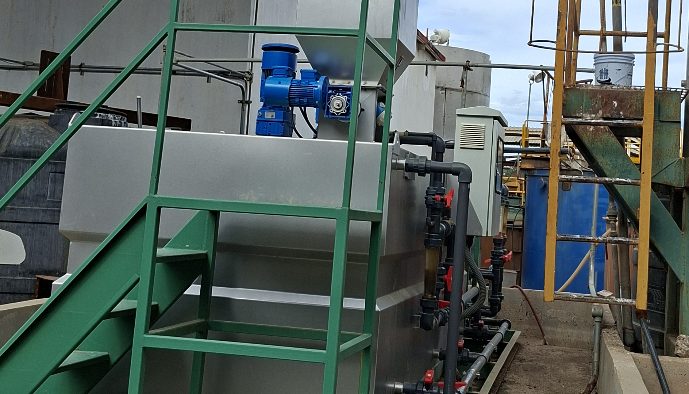
Cyanide is recovered for reuse, cutting fresh reagent consumption.
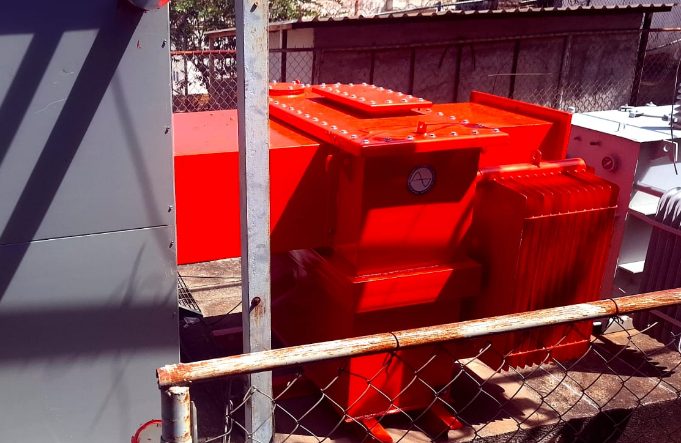
A new electrical substation, with a 750 kVA transformer and compact substation installed.
An expanded tailings filtering station, enabling dry-stacked tailings storage.
Tailings stored dry-stacked, rather than wet.
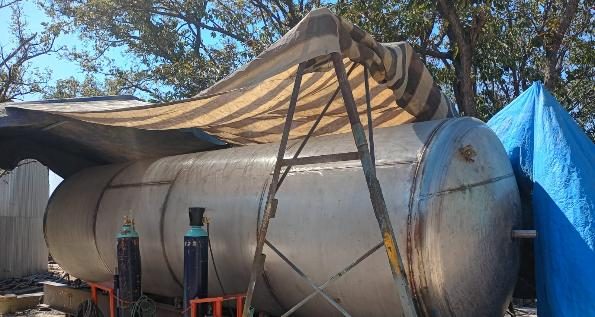
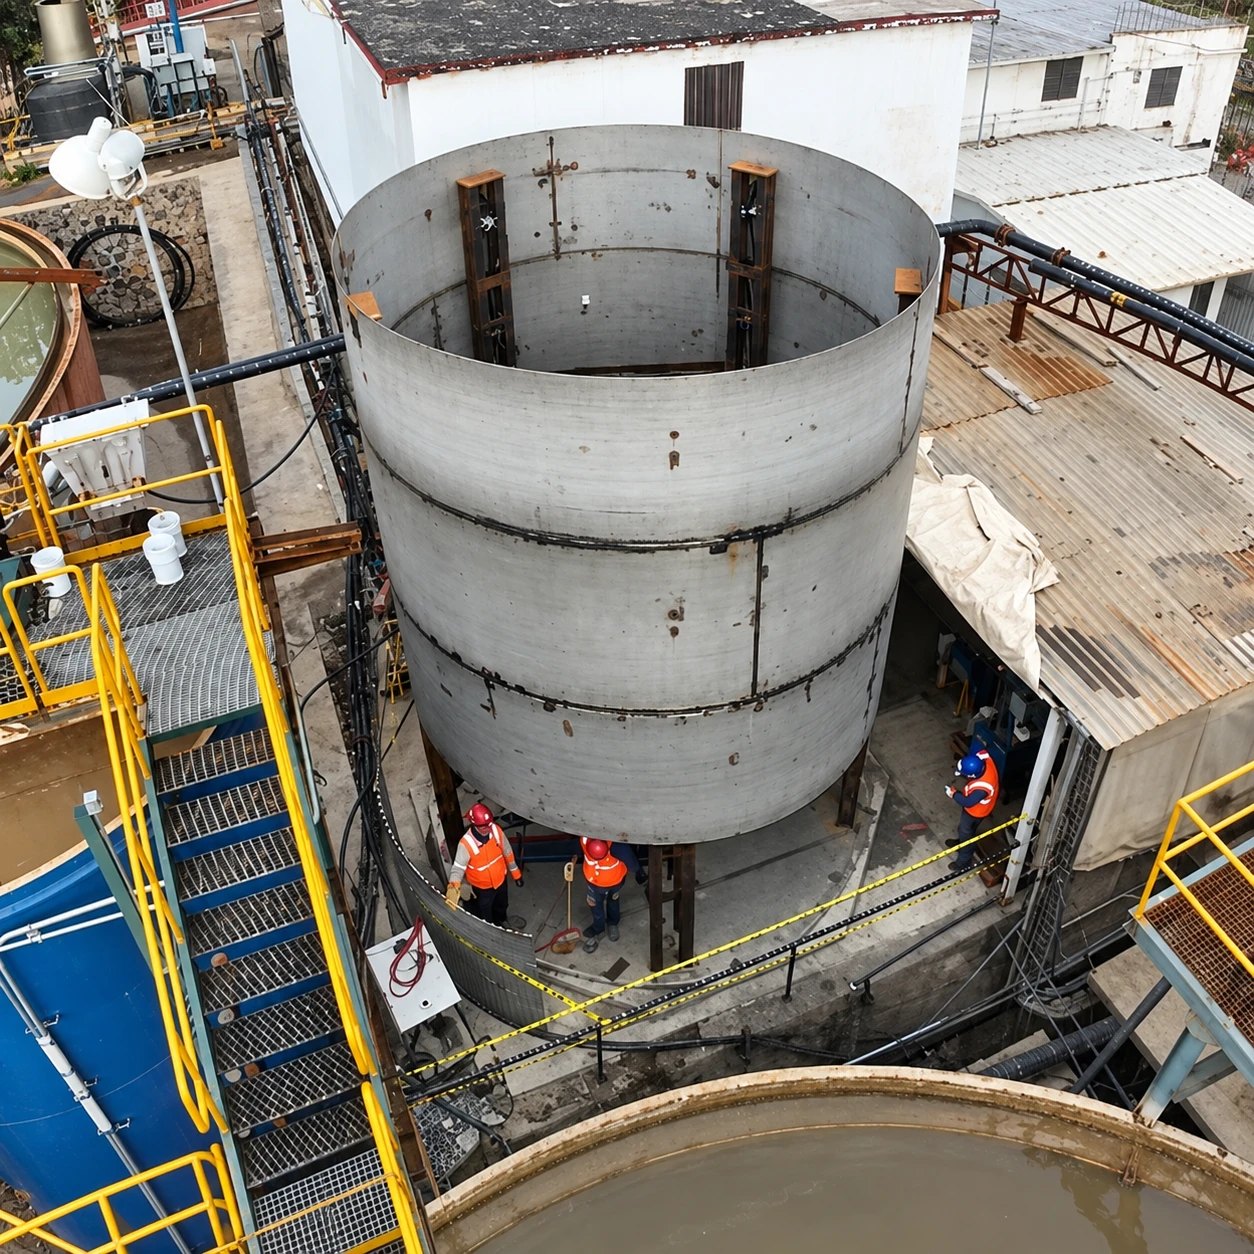
New stainless-steel process tanks, including two reagent tanks with stainless-steel piping and pumps, an acidity/basicity control tank, and a new 18,500-litre stainless-steel tank for ammonium bisulfite.
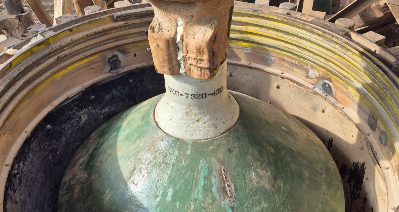
Primary, secondary and tertiary crushing circuits revamped, including repairs to the jaw crusher and the 4 ft and 3 ft cone crushers.
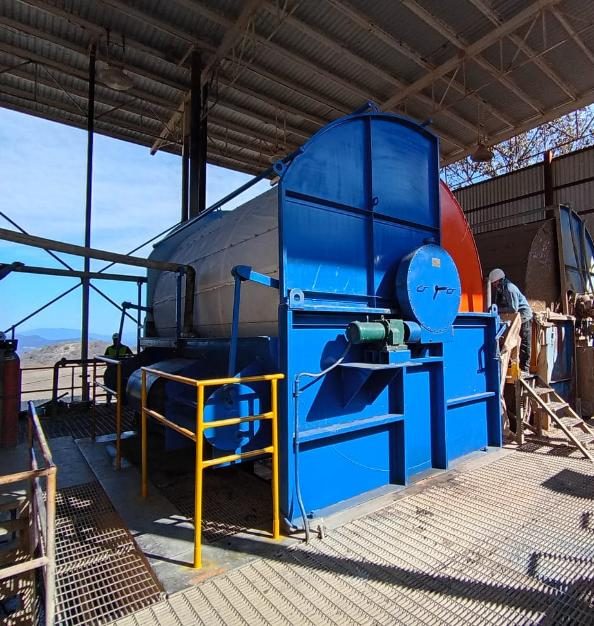
Existing drum filters fully rehabilitated. On vacuum filter no. 2, damaged steel was replaced, filter screens changed and the filter drive rebuilt.
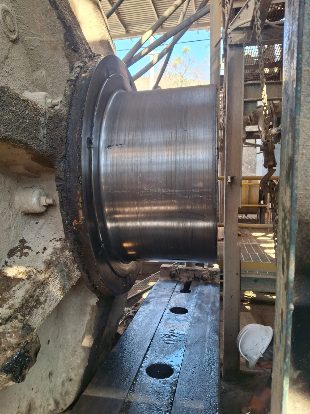
Babbitt bearing replaced on the 6′ × 12′ ball mill.
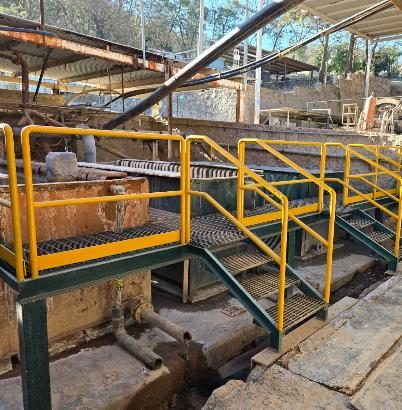
Two new Butters filters constructed for the precipitation circuit.
A micro-balance for weighing gold and silver installed and in operation.
New mucking and hauling equipment brought into the mine.
Mine water pumping stations rehabilitated, including cleaning of sump 018.
New pumps installed, including a 40 HP pump at sump 018.
Mine electrical systems upgraded.
Mine compressed-air systems upgraded.
After the 6′ × 5′ mill went out of service in October 2025, the company sourced a used 6′ × 6′ mill, rebuilt and installed it, with a corresponding slurry pump upgrade. It was commissioned and began operating in late December 2025.
A high-speed centrifugal decanter for liquid-solid separation, installed and started up, recovers water, residual values and cyanide for reuse.
Water is recovered by the centrifugal decanter for reuse.
Cyanide is recovered for reuse, cutting fresh reagent consumption.
A new electrical substation, with a 750 kVA transformer and compact substation installed.
An expanded tailings filtering station, enabling dry-stacked tailings storage.
Tailings stored dry-stacked, rather than wet.
New stainless-steel process tanks, including two reagent tanks with stainless-steel piping and pumps, an acidity/basicity control tank, and a new 18,500-litre stainless-steel tank for ammonium bisulfite.
Primary, secondary and tertiary crushing circuits revamped, including repairs to the jaw crusher and the 4 ft and 3 ft cone crushers.
Existing drum filters fully rehabilitated. On vacuum filter no. 2, damaged steel was replaced, filter screens changed and the filter drive rebuilt.
Babbitt bearing replaced on the 6′ × 12′ ball mill.
Two new Butters filters constructed for the precipitation circuit.
A micro-balance for weighing gold and silver installed and in operation.
Efficiency
The upgraded circuit adds pretreatment ahead of conventional cyanidation, recovers water and cyanide for reuse, and stores tailings dry-stacked rather than wet.
What changed
Also part of the upgraded operation: water and cyanide recovery for reuse, and a comprehensively revamped mine and plant.
The next phase
Reinvesting in people
Improved profitability has allowed the company to reinvest in its people, with a 25% increase to salaries that had been static for several years.
Investors